HDPE Pipe Machine Supplier Tips for Selecting High Performance Equipment
2026-10-12
Selecting an HDPE pipe machine is not just about picking the fastest or cheapest option on the market—it’s about finding equipment that will hold up under pressure, day after day. Yet many suppliers still gloss over the details that separate a workhorse from a costly mistake. From screw design to cooling efficiency, small engineering choices have a huge impact on extrusion quality and long-term operating costs. As one of the suppliers that keeps these details front and center, COMRISE has learned that true performance comes down to a few overlooked factors. In this guide, we’ll walk through the key criteria you should evaluate before committing to any high-performance HDPE pipe machine.
Start with Your Resin, Not the Brochure
Every resin behaves differently once it touches air, mold, or pigment. Instead of flipping through glossy pages filled with idealized cure times and perfect pours, grab a small batch and test it yourself. Notice how it thickens, where bubbles cling, and how it grabs color. Those quirks become your real working parameters.
Brochures promise consistency, but your studio temperature, humidity, and even the age of the bottle shift the outcome. By starting with the actual material in your hands, you learn to read its viscosity and exotherm instead of chasing numbers that rarely hold up in practice.
Let the resin teach you its own language. Mix a tiny cup without pigment, then another with a drop of alcohol ink. Watch how the surface seals, how it domes, how it shrinks. That direct observation builds a intuition no spec sheet can replace.
Ask for Live Run Data—Not Just Specs
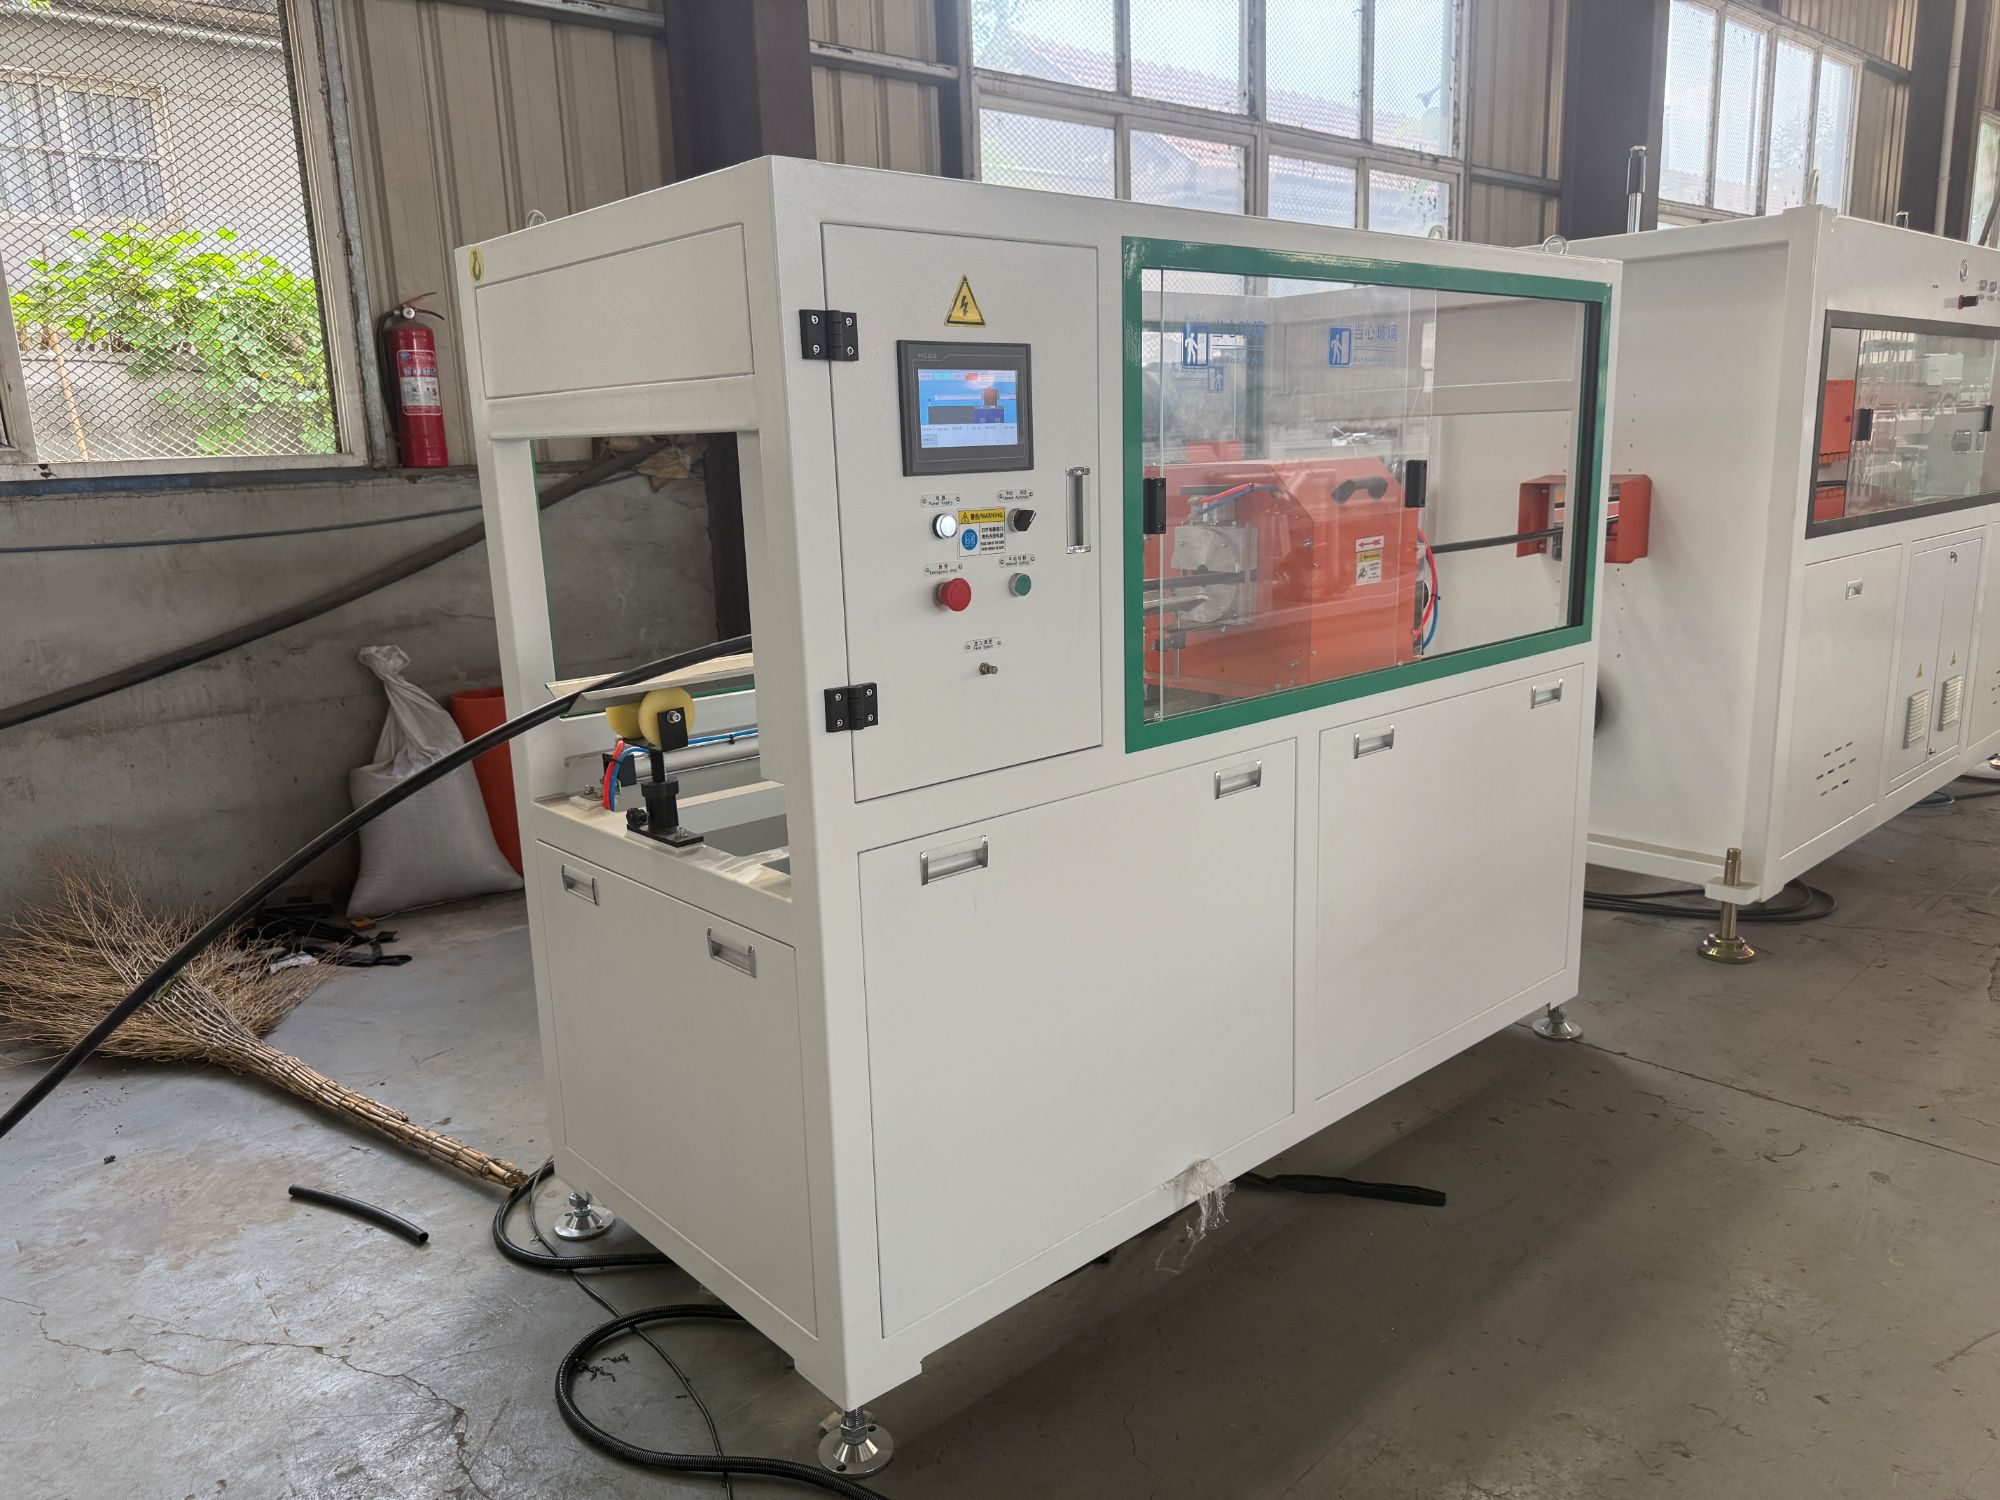
A spec sheet tells you what a machine was designed to do on its best day. Live run data tells you what it actually does on a random Tuesday, six months in, under a less-than-perfect operator. If you're comparing equipment, ask the vendor for real operational logs—not marketing summaries. Look for uptime percentages, average cycle times under real loads, and energy consumption measured from the field. Those numbers rarely match the brochure, and the gap is where hidden costs live.
Don't settle for a single cherry-picked case study. Request anonymized data from multiple installations with similar operating conditions to yours. Pay attention to how often components are replaced, how long the equipment sits idle for troubleshooting, and how performance degrades between service intervals. A vendor that hesitates to share this information is telling you something important—either the data doesn't exist, or it doesn't flatter the product.
When you get the data, compare it against the spec sheet side by side. Focus on variance: if the spec says 98% uptime but the field logs show 91%, ask why. That difference might come from ambient temperature, power quality, or operator training—all factors that will hit your operation too. Live run data is the closest thing to a test drive without renting the machine for a year. Use it to negotiate not just price, but service-level guarantees tied to real-world performance.
Dig Into the Screw and Barrel Metallurgy
The real story of a screw and barrel isn’t just geometry—it’s metal. A screw machined from soft steel will gall or snap under backpressure long before the flights wear out. Most modern screws start with 4140 alloy steel, then get case-hardened or nitrided to a surface hardness around 55–60 HRC. But that’s only the baseline. What matters is how the base metal, the hardening depth, and the barrel liner interact under heat, pressure, and aggressive fillers.
For abrasive or corrosive resins, you move into bimetallic barrels: a centrifugally cast lining of nickel-rich or tungsten carbide alloy inside a steel shell. The screw may be through-hardened with D2, coated with chrome oxide, or have welded hardfacing on the flight tips. This mismatch is critical—pairing a very hard barrel with a softer screw just shifts the wear to the screw root. A better approach is to match the wear couple so both sides degrade slowly and predictably.
Heat treatment details matter more than most spec sheets suggest. Deep cryogenic treatment after nitriding can convert retained austenite to martensite, improving fatigue life and dimensional stability. Checking microhardness across the barrel wall and along the screw root diameter will tell you more than a raw hardness number. That’s where processing stability is won or lost—not in the catalog description, but in the metallurgy under the surface.
Watch the Die Head During a Color Change
A color change is rarely as simple as feeding new pellets and waiting for the old shade to wash out. The die head is where the real story unfolds—it holds on to remnants like a stubborn stain in a fabric fold. If you stand back and trust the extruder to do all the work, you'll likely end up with streaks, off-spec parts, and wasted material. Get close to the die exit and watch how the melt behaves as the new color enters the flow path. The first sign of change is often a swirl of blended tones at the lip, then a gradual shift toward the target hue. That transition window is your best friend—don't rush it.
Look for telltale patterns on the extrudate surface. Thin, darker lines running along the length usually mean old compound is still shedding from a dead spot near the die land or a poorly swept corner. A marbled or cloudy appearance suggests the new color hasn't fully dispersed, especially if the change involves a big shift in pigment loading. Watch the die exit for any black specks or gel-like bumps that appear only when temperatures drift—those are often decayed material loosened by the higher heat needed for the new color. If you see the melt flickering or the parison wobbling slightly, it may be pressure variation from uneven melting, not just a cosmetic issue.
Keep a small mirror or a well-placed camera aimed at the die head so you can monitor the stream without leaning over hot surfaces. Many operators learn to read the sound of the extruder during a change—a steady, low groan usually means the screw is pushing clean material, while a rhythmic chug hints at surging. Write down how long the old color takes to clear at a given screw speed and temperature profile; that data saves you hours on the next switch. And remember, the die head has its own thermal inertia, so even after the extruder barrel looks clean, the lip may still hold the previous color for another minute or two. Trust your eyes more than the clock.
Compare Energy Draw at Rated Output
Manufacturers often list nominal wattage as a headline number, but actual draw at rated output can drift depending on load characteristics and ambient conditions. A unit that turns in an impressive peak figure may settle into a noticeably higher continuous draw once heat builds up, so side-by-side tests under the same rated load reveal more than spec sheets do.
When comparing two devices with identical rated output, differences of as little as five to ten watts per hour add up fast in daily use. That gap usually comes from inverter efficiency, cooling fan behavior, or how the control circuit manages transient demand. Short bench runs miss these patterns, so watching a stable meter over a thirty-minute window gives a clearer read.
If your priority is lower utility cost or longer battery runtime, rank candidates by draw at rated output rather than by maximum capability. The most efficient choice isn't always the one with the smallest power supply or the quietest fan; it's the one that holds the lowest average consumption while servicing the actual load you plan to run.
Find Out What Happens After the Warranty Ends
Once the manufacturer's warranty runs out, the safety net disappears. You might assume a product will still be repaired for free if it fails shortly after that date, but most companies draw a hard line. The moment the clock hits day one past the coverage period, labor and replacement parts become your expense—sometimes costing nearly as much as buying a new unit.
It's worth checking the fine print before that deadline sneaks up. Some brands quietly shift into a paid repair program where you can still get official service, but at full market rates plus shipping. Others won't touch out-of-warranty items at all and will point you toward independent shops. A few will offer a one-time discount on a new purchase if you call and ask, though they rarely advertise it.
Rather than waiting for something to break, pull up the original terms now. See whether the warranty covers parts and labor or just parts, and whether wear-and-tear items like batteries or belts are excluded. If an extended warranty is offered, do the math: compare its price against the likely repair cost and how long you actually plan to keep the product. A little digging can save you from an expensive surprise later.
FAQ
A good screw should handle the melt gently and maintain consistent output without excessive shear heat. Ask the supplier for the L/D ratio, compression ratio, and whether the screw geometry can be adjusted for different HDPE grades.
Ask for measured kilowatt-hours per kilogram of finished pipe, not just motor nameplate ratings. Reputable suppliers will share test data from recent installations and let you run your own material through their demo line.
The die head controls wall thickness uniformity and pressure distribution. A poorly designed spiral mandrel can create weld lines or uneven thickness, which leads to scrap and hidden quality issues once the pipe is in service.
Look for a PLC or industrial PC system with recipe storage, automatic temperature tuning, and real-time trending of melt pressure, motor load, and line speed. If the interface feels like an afterthought, the machine probably is too.
Yes. Seeing a machine running the same diameter and material you plan to use tells you more than any brochure. Pay attention to noise levels, vibration, and how clean the installation is—these reflect long-term build quality.
It's just as important as the extruder. Vacuum calibration tanks, cooling length, and haul-off stability determine whether you can hold tight tolerances at higher speeds. Weak downstream equipment will cap your output no matter how good the extruder is.
Find out where their spare parts warehouse is located, typical response time for a critical failure, and whether they offer remote diagnostics. Also ask for a list of common wear parts with local availability—not just what they can ship from overseas.
A flexible supplier will adapt the machine direction, cooling length, and cutting system to your space and the standards you need to meet, such as ISO or ASTM. If they only offer fixed configurations, you may end up paying for modifications later.
Conclusion
Choosing a high-performance HDPE pipe machine rarely starts with glossy brochures or horsepower numbers. It begins with the resin you actually run. Different molecular weights, recycled content, and additives change melt behavior enough that a machine tuned for one material can struggle with another. So the first question to any supplier should be about their experience with your specific formulation, not their general catalog. Once that matches, demand live run data from a comparable line rather than static spec sheets. Real throughput, melt temperature consistency, and pressure stability during a multi-hour trial tell you far more than a printed maximum output. Pay attention to the screw and barrel metallurgy too—coatings and alloys that resist wear from abrasive or corrosive regrind significantly extend service life and reduce downtime.
During a demonstration, stand by the die head during a color change. The speed and cleanliness of the transition reveal a lot about flow channel design and whether the head will cause costly scrap at every product switch. Energy draw at rated output is another number many buyers overlook until monthly utility bills arrive; compare kilowatts per kilogram across suppliers under identical conditions. Finally, ask what happens after the warranty expires. A supplier with a responsive service team, stocked spare parts, and a clear preventive maintenance schedule saves far more over ten years than a marginal upfront price difference. These six checks—resin fit, live data, metallurgy, die head behavior, energy efficiency, and post-warranty support—give you a practical framework for separating genuinely high-performance equipment from ordinary pipe machines wearing bold labels.
Contact Us
Contact Person: LISA LEE
Email: [email protected]
Tel/WhatsApp: +86 13780696467
Website: https://www.qdpipemachine.com