China CPP Film Masterbatch for Superior Film Quality and Processing Efficiency
2026-10-05
Ever wonder why some CPP film lines run flawlessly at high speed while others battle gel specks, haze, or poor dispersion? The secret rarely shows up in the resin data sheet—it hides in the masterbatch. A truly superior China CPP film masterbatch does more than add color; it optimizes melt flow, enhances film surface quality, and slashes energy consumption per kilogram. Xinwancai has built its reputation on exactly that kind of functional masterbatch engineering. Ready to see what your extrusion line has been missing?
Achieving Ultra-Low Haze Without Extra Cost
The pursuit of optical clarity often collides with budget constraints, but low haze doesn't have to demand a premium. By refining extrusion parameters and leveraging existing polymer grades, manufacturers can push haze below 0.5% using the same raw materials that were already in the pipeline. Small adjustments—like optimizing melt temperature profiles or fine-tuning cooling roll pressure—yield measurable clarity gains without adding a single cent to the bill of materials.
Conventional wisdom suggests that ultra-low haze films require specialized additives or higher-priced resins. In practice, the biggest wins come from eliminating micro-defects at the source: smoothing die lips, maintaining consistent web tension, and reducing gel contamination through better filtration. These process-level tweaks are often overlooked because they don't appear on a purchase order, yet they routinely outperform costly material swaps in side-by-side trials.
The key is treating haze as a symptom of processing variability rather than a material deficiency. When line operators monitor real-time optical feedback and adjust barrel temperatures within a narrow window, the same standard grade can achieve clarity levels once reserved for specialty films. No new additives, no reformulation—just tighter control over the variables that were already present.
Masterbatch Design That Prevents Gel Formation in CPP Extrusion
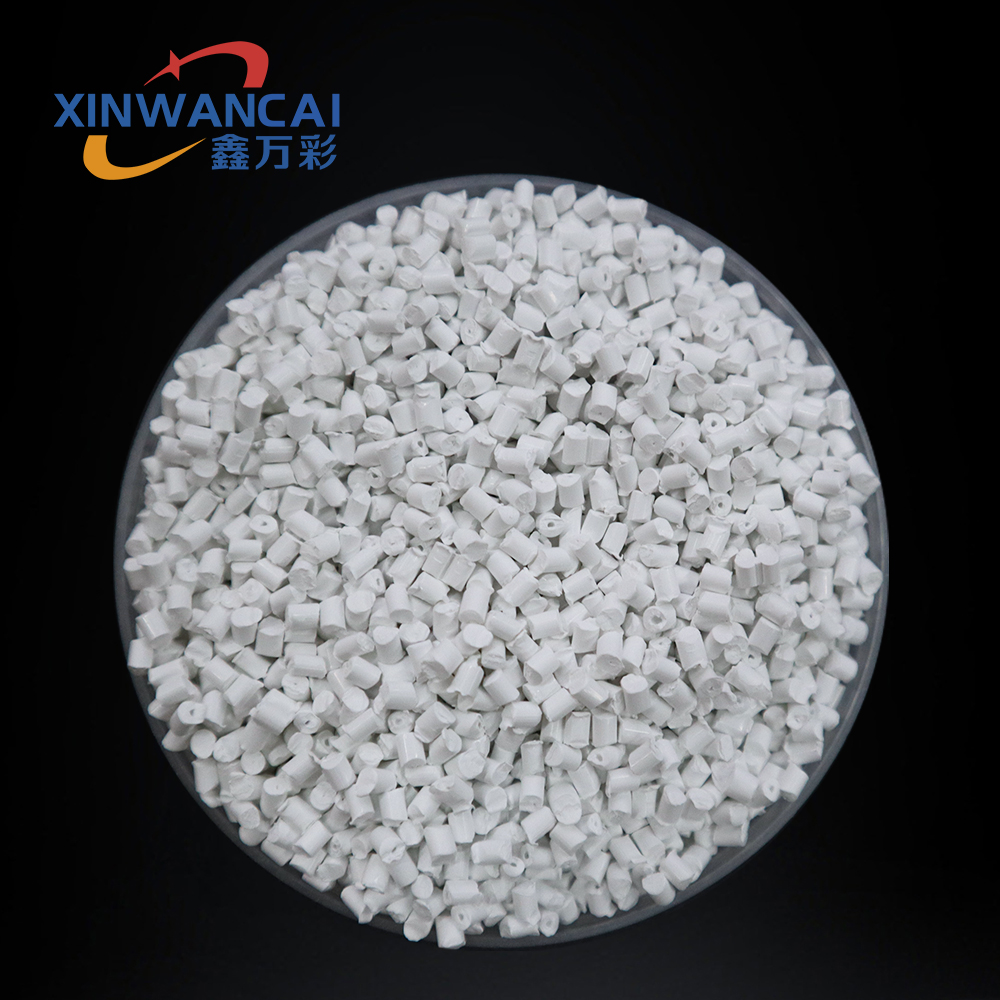
Gel formation during cast polypropylene film extrusion is rarely a single-cause problem, yet most masterbatch formulations still treat it as one. A well-designed masterbatch for CPP lines starts with the carrier resin, not the additive. Using a controlled-rheology polypropylene with a narrow molecular weight distribution reduces the low-molecular-weight tail that often degrades into crosslinked specks under high shear. The carrier should also have a melt flow index close to the base resin, so the masterbatch disperses without creating localized viscosity mismatches that lead to unmelted particles acting as gel nuclei.
The second layer of protection comes from the additive package itself. Instead of relying on a single high-load antioxidant, a synergistic blend of a hindered phenolic primary antioxidant and a phosphite secondary antioxidant works better. The phenolic catches free radicals during processing, while the phosphite decomposes hydroperoxides before they trigger chain scission or crosslinking. Crucially, the masterbatch should incorporate a small amount of an acid scavenger, such as calcium stearate or hydrotalcite, because residual catalyst residues from the base polypropylene can catalyze degradation under prolonged residence time in the die or screen pack.
Finally, pellet geometry and let-down ratio matter more than many processors realize. Spherical or near-spherical pellets with a diameter under 3 mm disperse faster and leave fewer unmelted cores compared to cylindrical pellets of the same weight. A let-down ratio between 2% and 4% forces the masterbatch through a long enough mixing section without over-concentrating the additives, which can itself cause gel spots from additive agglomeration. Running a purge test with a high-viscosity resin after each masterbatch change also helps flush out any partially degraded material from dead zones in the adapter or feedblock, where gels often originate even when the masterbatch is perfectly formulated.
Boosting Cast Line Speed Without Sacrificing Thickness Uniformity
Raising cast line speed usually creates a familiar trade-off: the film gets thinner at the edges or develops chatter marks because the melt has less time to settle before quenching. A more practical route starts with the die lip adjustment and air knife positioning, not just the drive motor. Small, deliberate changes to the primary chill roll gap and vacuum box pressure keep the web pinned evenly as it accelerates, so the polymer freezes before gravity or drag can redistribute it.
Another overlooked variable is melt temperature stability. When speed climbs, shear heating inside the extruder can shift viscosity by a few percent, and that is enough to change draw resonance. Tightening the barrel zone profile and using a melt pump with a steady discharge pressure often does more for gauge consistency than slowing back down. Operators who track thickness profiles at multiple points across the web can spot a repeating high or low band early and correct it with a nudge to the flex lip bolts rather than accepting the usual speed limit.
Finally, consider the quench side. A higher line speed demands faster heat removal, but simply cranking up chill roll cooling can cause uneven contraction if the roll surface temperature varies more than a degree or two. Keeping coolant flow balanced across the roll and polishing the surface to remove microscopic scale keeps the contact area uniform. Paired with a closed-loop thickness gauge that feeds back to the die bolts every few seconds, it is possible to run significantly faster without seeing the edge beads and transverse variation that usually come with it.
Chinese CPP Masterbatch: Where Local R&D Meets Global Film Demands
Chinese CPP masterbatch producers have moved well beyond being generic additive suppliers. Over the past decade, local R&D teams have dug deep into cast polypropylene film processing behavior, creating formulations tailored to specific line speeds, heat-seal temperatures, and haze targets. For example, some companies now offer anti-blocking masterbatches that run smoothly on high-speed cast lines exceeding 200 meters per minute while keeping film haze below 1.5%.
Global film demand is shifting toward thinner, clearer packaging, which forces CPP masterbatches to improve in dispersion and compatibility. Chinese researchers work closely with domestic resin suppliers and equipment makers, cutting the time from lab trials to commercial production. A typical case is masterbatch for metallized CPP film, where formulators must reduce surface migration without sacrificing metal adhesion—a delicate balancing act.
This is no longer a story of low-cost imitation. Chinese manufacturers are offering customized masterbatches to converters in Southeast Asia, the Middle East, and Europe, iterating quickly on slip agents, antiblock levels, and optical properties. Some companies even run downstream application tests in parallel with their customers' trials. That market-driven R&D approach is repositioning Chinese CPP masterbatch from an alternative supplier to a co-developer.
Custom Slip and Antiblock Packages for Trouble-Free Converting
Custom slip and antiblock packages start with a clear read of your converting line: film gauge, haul-off speed, winding tension, and the exact resin blend you run. Rather than forcing a one-size-fits-all additive ratio, the package is built around those variables so the film releases cleanly from the roll, keeps a stable coefficient of friction, and does not build up static or dust at the die or in the slitting area.
The real problem in most converting stops is not the film itself but a mismatch between slip migration and antiblock particle size. For thin-gauge PE or PP, we adjust the slip package to bloom at a controlled rate, so the surface stays easy to move without becoming hazy or hurting heat-seal strength. At the same time, the antiblock grade is selected for its particle shape and size distribution, which prevents micro-scratching on high-clarity webs and keeps reel edges from telescoping.
Because every line drifts over time—temperature swings, recycled content changes, new die gap settings—the package includes a quick revision path. Instead of re-qualifying a full formulation, you adjust one component, and the change is documented against your roll-stock performance data. That way the converting floor keeps running with fewer stops, lower scrap, and no guesswork at the winder.
Why Masterbatch Purity Directly Affects Seal Integrity
In flexible packaging, the seal layer is often the last line of defense against moisture, oxygen, and contamination. When masterbatch is added to the polymer, any impurity it carries—whether residual catalysts, unpolymerized monomers, or foreign particles—can migrate to the seal interface during extrusion and weaken the bond. These contaminants act as stress concentrators or create micro-voids that lower the peel strength and make the seal more prone to channel leaks. Over time, a slightly compromised seal may pass initial QC but fail in real-world distribution, especially under fluctuating temperatures or rough handling.
The purity of the masterbatch also influences how evenly the carrier resin disperses into the base polymer. Low-grade masterbatch often contains gels or agglomerated pigment clusters that disrupt the smooth film surface at the sealant layer. These irregularities cause uneven heat transfer during the sealing jaw dwell, resulting in weak spots where the two film layers do not fully fuse. In contrast, a high-purity masterbatch maintains a consistent melt viscosity and particle size distribution, allowing the sealant to flow uniformly and form a continuous, high-integrity bond across the entire seal width.
Beyond physical contamination, chemical impurities in masterbatch—such as acidic residues or low-molecular-weight waxes—can interact with the polymer chain during extrusion. These species may degrade the molecular weight of the sealant resin or modify its crystallization behavior, reducing the hot tack strength and increasing the minimum sealing temperature. In demanding applications like retort pouches or vacuum packaging, even a 2–3% drop in seal strength due to impurity-related degradation can lead to field failures. Thus, selecting a masterbatch with documented purity levels is not a cosmetic choice; it directly determines whether the final seal will hold up under pressure, heat, and sustained load.
FAQ
A high-quality CPP masterbatch is formulated with carefully selected carrier resins and additives that disperse uniformly at low addition rates. This prevents visible gels, fisheyes, and uneven thickness in cast film, which standard compounds often struggle with. The difference shows up most in film clarity, seal strength, and how consistently the line runs without screen pack clogging.
It reduces torque and melt pressure by improving internal lubrication during extrusion. That allows higher line speeds without overheating the melt, which means less energy per kilogram of film and fewer breaks during edge trimming or winding. Operators also notice fewer die lip deposits, so shutdowns for cleaning become less frequent.
Slip and anti-block agents usually make the most immediate difference. A well-balanced masterbatch delivers controlled migration of slip additives to the film surface, giving stable coefficient of friction without blooming too fast. Anti-block particles must be small and uniformly dispersed to prevent haze while still allowing easy film separation.
Yes, because it supports better melt strength and gauge uniformity. With a consistent melt and fewer thickness variations, processors can reduce film thickness while maintaining dart impact and seal integrity. The key is using a masterbatch that does not introduce stress concentration points from poorly dispersed particles.
Look beyond the datasheet. Request trial data on gel count, filter pressure rise, and coefficient of friction stability over time. A reliable supplier will also offer consistent lot-to-lot additive loading and be willing to adjust formulations for specific resins or line conditions.
The carrier should match the base polypropylene closely in melt flow rate and crystallinity. If the carrier is too different, it can create local weak spots or haze bands. A compatible carrier ensures the additives are distributed evenly and do not interfere with the film's thermal or optical properties.
Yes, some masterbatches are designed to minimize low-molecular-weight components that can cause surface defects or affect metal adhesion. These grades focus on very clean formulations with low volatiles, which improves metal bond strength and reduces the risk of pinholes after metallization.
It can help with film blocking on the roll, poor slip causing wrinkles during slitting, die build-up, and unstable bubble or cast roll contact. By addressing dispersion and additive compatibility, it also reduces screen pack changes and keeps output rates steady over long runs.
Conclusion
Chinese CPP film masterbatch now resolves several long-standing production bottlenecks within a single carrier system. Instead of accepting higher haze as a trade-off for lower cost, converters can reach ultra-low haze through optimized pigment and additive dispersion, without raising formulation expense. The masterbatch design also suppresses gel formation during CPP extrusion—gel specks remain a common source of film defects and unplanned downtime. At the same time, the right masterbatch allows cast lines to run faster while preserving thickness uniformity across wide webs, which raises throughput without compromising gauge consistency. This integrated approach reduces the need for secondary corrective additives and keeps total formulation cost stable.
Local R&D in China has moved beyond simple cost-driven production. These masterbatches are increasingly tuned to global film requirements: custom slip and antiblock packages support trouble-free converting in printing, laminating, and bag-making, reducing blocking and friction without overdosing additives. Purity control acts as another key differentiator—low levels of residual catalysts, moisture, and fine contaminants help maintain seal integrity, especially on high-speed packaging lines where weak seals cause rejects. By combining these properties, Chinese CPP masterbatches offer a practical route to better opticals, smoother extrusion, and more reliable downstream processing. Film producers no longer need to choose between optical clarity, line productivity, and reliable sealing performance.
Contact Us
Contact Person: JACK
Email: [email protected]
Tel/WhatsApp: 86 18650130917
Website: https://www.xinwancai.com/